Most plants trying to improve OEE start in the wrong place. They push operators to run faster or chase scrap, while the biggest losses sit in the maintenance log: breakdowns, long repairs, slow changeovers and the small stoppages nobody records.
OEE (overall equipment effectiveness) multiplies three factors: availability, performance and quality. Maintenance controls most of the first and a large share of the other two. If your OEE has been stuck at 55–65% for a year, the fastest way up is usually not a new production target. It is fewer breakdowns, faster repairs and better-planned maintenance.
This guide shows exactly which OEE losses come from maintenance, how much a small cut in downtime lifts OEE (with a worked example), and seven practical ways to improve OEE through maintenance. If you want to see where your own plant is losing OEE, you can book a free 30-minute PlantOps360 demo at any point.
OEE in one minute
OEE tells you what share of your planned production time produced good parts at full speed. A score of 100% means no stops, no slow running and no defects.
OEE = Availability × Performance × Quality
- Availability = run time ÷ planned production time. It drops with breakdowns, changeovers and other stops.
- Performance = (ideal cycle time × total count) ÷ run time. It drops with slow running and minor stoppages.
- Quality = good count ÷ total count. It drops with scrap, rework and start-up rejects.
The widely quoted world-class OEE benchmark is 85% (roughly 90% availability, 95% performance and 99.9% quality), a figure from Seiichi Nakajima's work on Total Productive Maintenance (TPM). Many plants that measure honestly find they sit between 40% and 60%.
For the step-by-step calculation, see our OEE calculation guide. This article focuses on the next question: how do you actually raise it?
The six big losses: which ones maintenance controls
TPM groups every OEE loss into six "big losses". Maintenance is the main cause of three of them and a contributor to the other three.
| Big loss | OEE factor hit | Typical maintenance cause | How maintenance fixes it | Maintenance influence |
|---|---|---|---|---|
| Equipment breakdowns | Availability | Worn bearings, seals, belts; missed PMs; no early warning | Preventive and predictive maintenance, faster repairs | High |
| Setup and changeover | Availability | Missing tools or spares, unclear procedures, adjustments | Standard checklists, spares kitted in advance, SOPs at the machine | Medium |
| Minor stops (idling, jams) | Performance | Misaligned guides, dirty sensors, worn parts | Logging stops, root-cause fixes, cleaning and inspection routines | High |
| Reduced speed | Performance | Machines run slow to avoid breakdowns; poor lubrication, wear | Restoring equipment to its design condition | High |
| Start-up rejects | Quality | Unstable machine after a stop or repair | Better repair quality, warm-up checklists, calibration | Medium |
| Production rejects | Quality | Drifting instruments, worn tooling | Calibration schedules, tooling PMs | Medium |
Read the table from the left. Breakdowns, minor stops and reduced speed are often the three biggest OEE losses in a plant, and all three are equipment-condition problems. That is why a reliable maintenance system tends to move OEE more than any production campaign.
Worked example: what 20 fewer minutes of breakdown does to OEE
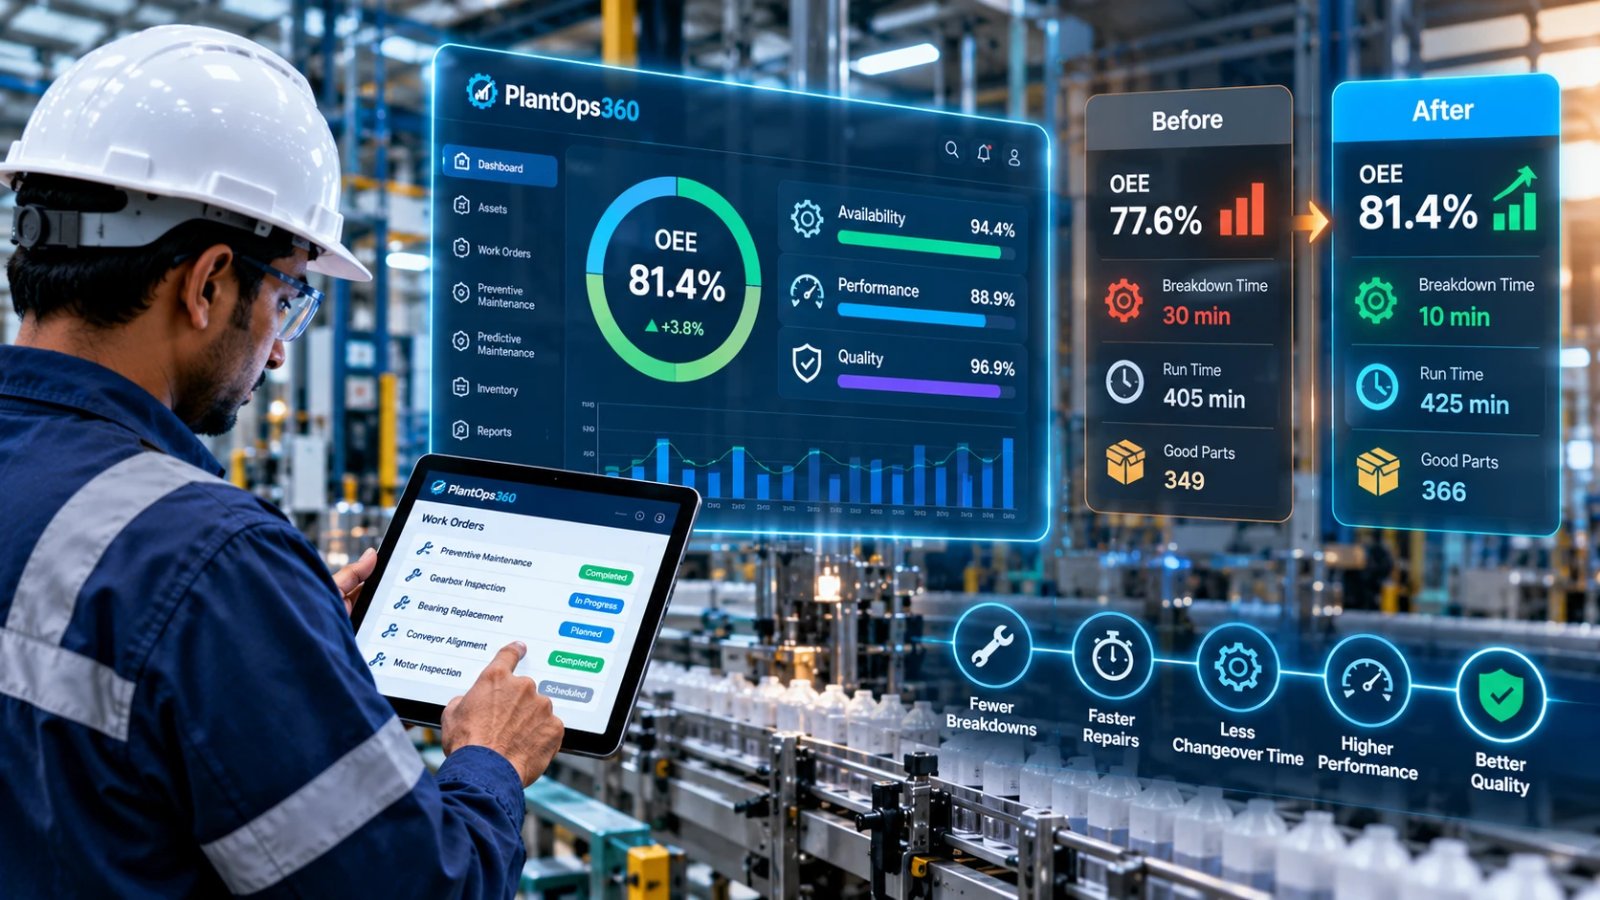
Cutting breakdown time by 20 minutes a shift lifts this line's OEE from 77.6% to 81.4%, about 17 extra good parts every shift, without touching speed or quality.
Take one packing line on an 8-hour shift with a 30-minute break, so 450 minutes of planned production time. The ideal rate is 60 parts an hour (one part a minute). Changeovers take 15 minutes a shift.
| Before | After better maintenance | |
|---|---|---|
| Breakdown time per shift | 30 min | 10 min |
| Run time (450 − breakdowns − 15 min changeover) | 405 min | 425 min |
| Availability | 90.0% | 94.4% |
| Performance (same running speed) | 88.9% | 88.9% |
| Quality (same reject rate) | 96.9% | 96.9% |
| Good parts per shift | 349 | 366 |
| OEE | 77.6% | 81.4% |
Over three shifts a day and 300 working days, those 17 parts add up to roughly 15,000 extra good parts a year from the same machine, the same crew and no capital spend.
In real plants the gain is usually bigger. Machines that break down less also run closer to their design speed and make fewer start-up rejects, so performance and quality tend to rise with availability.
Why OEE stalls in plants that run reactive maintenance
OEE stops improving when the plant can see that it lost time but not why. Four patterns show up again and again.
Downtime is recorded, causes are not. The production log says "Line 3 down 40 minutes". The maintenance record, if there is one, says "fixed". Nobody can tell that the same gearbox failed four times this quarter.
Minor stops are invisible. Two-minute jams don't make it into any register. Twenty of them a shift is 40 minutes of lost performance that never gets a work order.
PMs slip when production is busy. The first thing dropped in a rush week is the inspection that would have caught next week's breakdown.
Repairs wait on people and parts. Technicians hunt for the right spare, the manual or the person who fixed it last time. Every minute of that waiting is availability loss.
None of these is a production problem. Each one is a maintenance data and discipline problem, which is exactly what a CMMS is built to fix.
7 ways to improve OEE through maintenance
Start with the bottleneck machine, the one whose downtime stops the whole line, and work down this list.
1. Record every stop with a reason and a failure code
You cannot reduce what you do not measure. Every breakdown and every repeated minor stop should end in a work order with the asset, the failure code, the cause and the downtime minutes. After a month you will know which three assets and which three failure modes cost you the most OEE.
2. Make preventive maintenance non-negotiable on critical assets
Schedule PMs by calendar, runtime or meter reading, and track PM compliance weekly. Protect the PM window on the production plan the same way you protect a customer order. Missed PMs on the bottleneck should be a management conversation, not a footnote.
3. Move critical assets to condition-based and predictive maintenance
For motors, pumps, compressors and gearboxes, vibration, temperature and current readings warn of failure days or weeks ahead. Predictive maintenance turns a surprise breakdown (availability loss) into a planned stop during a changeover or a weekend.
4. Cut mean time to repair (MTTR)
Every minute between "machine down" and "machine running" is availability you lose. Shorten it with instant breakdown alerts, the asset's repair history on the technician's phone, the right spares already in stock, and the manual or SOP one tap away.
5. Attack minor stops and reduced speed
Minor stops and slow running are performance losses that hide in plain sight. Log them, group them by cause, and fix the top causes at the root: realign the guide rail, replace the worn part, clean the sensor. Then restore the machine to its rated speed.
6. Standardise changeovers
Create a changeover checklist for each product switch, kit the parts and tools before the line stops, and record changeover time as its own downtime category. SMED (single-minute exchange of dies) principles work best when maintenance prepares the equipment in advance.
7. Keep instruments and tooling calibrated
Drifting gauges and worn tooling create quality losses that look like operator error. A calibration schedule with due-date alerts and recorded results protects the quality factor, and keeps you audit-ready.
Track OEE alongside MTBF and MTTR
OEE tells you how much you lost; MTBF and MTTR tell maintenance why. Track them side by side for the same assets.
| Metric | What it answers | Moves which OEE factor |
|---|---|---|
| MTBF (mean time between failures) | How often does this asset break down? | Availability |
| MTTR (mean time to repair) | How long does each breakdown last? | Availability |
| PM compliance | Are we doing the maintenance we planned? | Availability, performance |
| Planned vs unplanned work ratio | Are we in control or firefighting? | All three |
| Repeat failure rate | Are our fixes lasting? | Availability |
A simple rule: if availability is your weakest OEE factor, look at MTBF first (too many failures) and MTTR second (repairs too slow). Our guide to MTTR and MTBF formulas shows how to calculate both.
How PlantOps360 helps you raise OEE
PlantOps360 is an AI-powered CMMS and EAM that attacks the maintenance side of OEE: fewer breakdowns, faster repairs and maintenance data you can act on.
| OEE loss | What PlantOps360 does |
|---|---|
| Breakdowns | Preventive maintenance scheduled by time, usage or meter reading, with PM compliance and MTBF tracked in real time |
| Breakdowns you didn't see coming | AI predictive maintenance turns sensor, IIoT and maintenance-history data into early failure warnings |
| Slow repairs (high MTTR) | Work orders raised by QR scan, an AI copilot that auto-fills failure codes and suggests parts and SOPs, and a mobile app that works offline |
| Waiting for spares | Spare parts and MRO inventory linked to each asset |
| Quality drift | Calibration management with due dates and recorded results |
| No idea where the losses are | Dashboards for MTTR, MTBF and failure trends, plus plain-English questions answered with charts |
Find the downtime that is eating your OEE
In a free 30-minute demo, we will:
- Show how a breakdown becomes a work order with its cause, downtime and parts recorded.
- Walk through MTTR, MTBF and failure-trend dashboards on a plant like yours.
- Pick the bottleneck assets where better maintenance would lift your OEE fastest.
Book your free OEE and maintenance demo
Frequently asked questions
How can maintenance improve OEE?
Maintenance improves OEE mainly through availability: fewer breakdowns through preventive and predictive maintenance, and shorter repairs through faster response, ready spares and repair history at hand. Well-maintained machines also run closer to rated speed and make fewer rejects, which lifts performance and quality.
Which OEE factor does maintenance affect most?
Availability. Breakdowns and long repairs are availability losses, and they are usually the largest single loss on a production line.
What is a good OEE score?
85% is the widely quoted world-class benchmark. Around 60% is common for plants just starting to measure. The useful target is steady improvement on your own bottleneck, not a number from another industry.
What are the six big losses in OEE?
Breakdowns, setup and changeovers (availability); minor stops and reduced speed (performance); start-up rejects and production rejects (quality).
How does a CMMS improve OEE?
A CMMS schedules and enforces preventive maintenance, records every breakdown with its cause and downtime, speeds up repairs with mobile work orders and spare-parts tracking, and shows MTBF and MTTR so you can fix the assets that hurt OEE most.
How does predictive maintenance improve OEE?
Predictive maintenance spots early warning signs in vibration, temperature or current data, so a failure becomes a planned job in a scheduled stop. Unplanned downtime falls, and availability rises.
What is the relationship between OEE, MTBF and MTTR?
Availability depends on how often equipment fails (MTBF) and how long each repair takes (MTTR). Raise MTBF or cut MTTR and availability, and therefore OEE, goes up.
What is TPM and how does it relate to OEE?
Total Productive Maintenance (TPM) is a method that involves operators and maintenance teams in keeping equipment in top condition. OEE is TPM's main measure of success.
How fast can we improve OEE through maintenance?
Plants that start recording downtime causes usually find their top repeat failures within the first month. Fixing those and protecting PMs on the bottleneck can show OEE gains within one or two quarters.
The bottom line
If you want higher OEE, look at your maintenance log before your production targets. Breakdowns, slow repairs, minor stops and machines running below rated speed are maintenance problems, and they are where most plants lose the bulk of their OEE.
Record every stop with its cause, protect PMs on the bottleneck, add early warning on critical rotating equipment, and cut the time it takes to get a machine running again. As the worked example shows, 20 fewer minutes of breakdown a shift is worth almost 4 OEE points.
Want to see where your plant is losing OEE? Book a free 30-minute PlantOps360 demo and we will show you how to find and fix the maintenance losses holding your OEE back.