OEE (overall equipment effectiveness) is the share of planned production time that turns into good parts at full speed. You calculate it as Availability × Performance × Quality, or more simply as good count × ideal cycle time ÷ planned production time.
This guide walks through the OEE calculation step by step with a worked example, gives you a ready layout for an OEE calculation in Excel, explains what a good OEE score is, and lists the mistakes that make OEE numbers look better (or worse) than reality. It is written for maintenance and production teams who need a number they can trust and act on.
The five numbers you need to calculate OEE
Every OEE calculation uses the same five inputs, collected for one machine or line over one period (a shift, a day, a week).
| Input | What it means | Where it usually comes from |
|---|---|---|
| Planned production time | Shift time minus planned stops (breaks, meetings, scheduled maintenance) | Shift plan |
| Downtime | Unplanned and setup stops: breakdowns, changeovers, waiting for material | Downtime log, CMMS work orders |
| Ideal cycle time | Fastest time to make one part under ideal conditions | Machine spec or best demonstrated rate |
| Total count | Every part produced, good or bad | Machine counter, production report |
| Good count | Parts that pass first time, with no rework | Quality records |
Run time = planned production time − downtime. It feeds both availability and performance.
How to calculate OEE, step by step
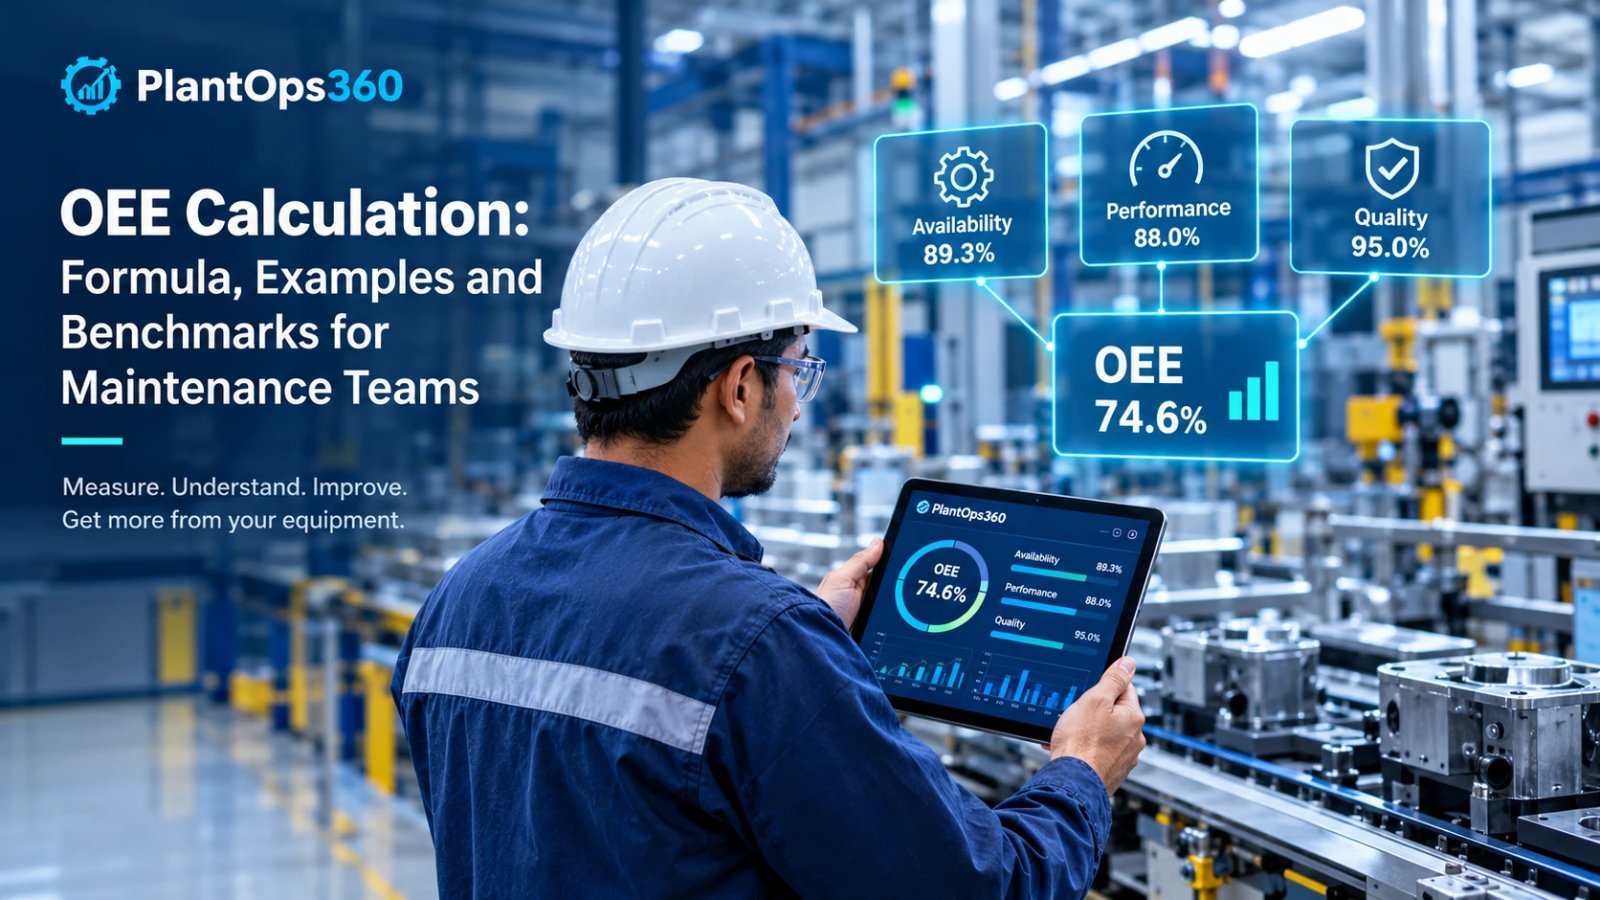
This CNC machine's OEE works out to 74.6% for the shift. Here is how.
The shift: 8 hours (480 minutes), with a 30-minute break and 30 minutes of scheduled maintenance. During the shift the machine broke down for 25 minutes and spent 20 minutes on a changeover. The ideal cycle time is 1.5 minutes per part. It made 220 parts, of which 209 were good.
Step 1: Planned production time
Planned production time = 480 − 30 (break) − 30 (scheduled maintenance) = 420 minutes
Step 2: Run time and availability
Run time = 420 − 25 (breakdown) − 20 (changeover) = 375 minutes
Availability = 375 ÷ 420 = 89.3%
Step 3: Performance
Performance = (1.5 × 220) ÷ 375 = 330 ÷ 375 = 88.0%
The machine could have made 250 parts in 375 minutes at ideal speed. It made 220, so slow running and minor stops cost 12% of its performance.
Step 4: Quality
Quality = 209 ÷ 220 = 95.0%
Step 5: OEE
OEE = 89.3% × 88.0% × 95.0% = 74.6%
| Factor | Calculation | Result |
|---|---|---|
| Availability | 375 ÷ 420 | 89.3% |
| Performance | (1.5 × 220) ÷ 375 | 88.0% |
| Quality | 209 ÷ 220 | 95.0% |
| OEE | 89.3% × 88.0% × 95.0% | 74.6% |
The weakest factor tells you where to look first. Here availability and performance are close, so both the 25-minute breakdown and the lost speed deserve attention.
The quick OEE formula, and an Excel template
If you only need the OEE score, one formula gives the same answer:
OEE = (Good count × Ideal cycle time) ÷ Planned production time
For the example above: (209 × 1.5) ÷ 420 = 313.5 ÷ 420 = 74.6%. Use the three-factor method whenever you want to know why OEE is low.
OEE calculation in Excel
Set up one sheet like this and copy it for each machine or shift. Format B8 to B11 as percentages.
| Cell | Label | Example value | Formula |
|---|---|---|---|
| B2 | Planned production time (min) | 420 | entered |
| B3 | Downtime (min) | 45 | entered |
| B4 | Ideal cycle time (min/part) | 1.5 | entered |
| B5 | Total count | 220 | entered |
| B6 | Good count | 209 | entered |
| B7 | Run time (min) | 375 | =B2-B3 |
| B8 | Availability | 89.3% | =B7/B2 |
| B9 | Performance | 88.0% | =(B4*B5)/B7 |
| B10 | Quality | 95.0% | =B6/B5 |
| B11 | OEE | 74.6% | =B8*B9*B10 |
A spreadsheet works for one machine. Across a plant, the hard part is not the formula; it is getting honest downtime and reject data into it every shift.
What is a good OEE score?
The widely quoted world-class OEE is 85%, but the target that matters is steady improvement on your own bottleneck.
| OEE score | What it usually means |
|---|---|
| 100% | Perfect production: no stops, full speed, no defects. A theoretical ceiling. |
| 85% | World class for discrete manufacturing (from Seiichi Nakajima's TPM work) |
| 60% | Typical for plants that have started measuring and improving |
| 40% or less | Common when OEE is first measured; large, easy gains available |
The 85% benchmark breaks down as roughly 90% availability, 95% performance and 99.9% quality (90% × 95% × 99.9% = 85.4%). Notice that availability is the lowest of the three, which is why maintenance is so central to world-class OEE.
Compare OEE over time on the same machine rather than across different machines or industries. A packaging line and a CNC cell will never have the same "good" score.
OEE vs TEEP vs availability
These three terms are often mixed up. They answer different questions.
| Metric | Formula | Answers |
|---|---|---|
| Availability | Run time ÷ planned production time | How much of the planned time was the machine actually running? |
| OEE | Availability × Performance × Quality | How well did we use the time we planned to produce? |
| TEEP (total effective equipment performance) | OEE × utilisation (planned production time ÷ all calendar time) | How much of the machine's total 24/7 capacity did we turn into good parts? |
In the example, the machine runs one 420-minute shift a day. Utilisation is 420 ÷ 1,440 = 29.2%, so TEEP = 74.6% × 29.2% = 21.8%. TEEP shows how much hidden capacity a second or third shift could unlock before you buy another machine.
Common OEE calculation mistakes
Most wrong OEE numbers come from the inputs, not the formula. Watch for these six.
- Using a slow "standard" cycle time instead of the ideal one. A padded cycle time hides speed losses and can push performance above 100%. Use the machine's design speed or best demonstrated rate.
- Not recording minor stops. Short jams that nobody logs disappear into performance. If performance looks low with no explanation, minor stops are the usual cause.
- Counting reworked parts as good. Quality should count only parts that are right first time.
- Treating changeovers as planned time. Changeovers are an availability loss you can reduce. Excluding them makes OEE look better while hiding a real improvement opportunity.
- Being inconsistent about scheduled maintenance. Decide once whether planned maintenance counts as planned stop time or downtime, document it, and apply it everywhere. Otherwise OEE moves when nothing has changed.
- Averaging OEE across the whole plant. A plant-wide average hides the bottleneck. Calculate OEE per machine or line, and focus on the constraint.
Accurate OEE starts with maintenance data
You can only improve OEE if you know why the time was lost, and most of those answers live in maintenance records.
PlantOps360, an AI-powered CMMS and EAM, captures the maintenance side of every OEE loss:
- Every breakdown recorded with its cause. Work orders raised by QR scan, with an AI copilot that auto-fills failure codes.
- Fewer breakdowns. Preventive maintenance by time, usage or meter reading, with PM compliance and MTBF tracked in real time.
- Early warning. AI predictive maintenance turns sensor, IIoT and maintenance-history data into failure warnings.
- Faster repairs. A mobile app that works offline, with asset history, parts and SOPs at the machine.
- Clear trends. Dashboards for MTTR, MTBF and failure trends, and plain-English questions answered with charts.
Once you know your OEE, the next question is how to raise it. Our guide on how to improve OEE through maintenance covers the six big losses and seven practical fixes.
Book a free 30-minute PlantOps360 demo to see how your maintenance data can explain, and lift, your OEE.
Frequently asked questions
What is the formula for OEE?
OEE = Availability × Performance × Quality. The short version is OEE = (good count × ideal cycle time) ÷ planned production time. Both give the same result.
How do you calculate availability in OEE?
Availability = run time ÷ planned production time, where run time is planned production time minus downtime (breakdowns, changeovers and other stops).
How do you calculate performance in OEE?
Performance = (ideal cycle time × total count) ÷ run time. It shows how close the machine ran to its ideal speed while it was running.
How do you calculate quality in OEE?
Quality = good count ÷ total count. Count only parts that are right first time.
What is the full form of OEE?
OEE stands for overall equipment effectiveness.
What is a good OEE percentage?
85% is considered world class. Around 60% is typical for plants that are actively improving, and 40% is common when OEE is first measured.
Can OEE be more than 100%?
No. If your OEE is above 100%, the ideal cycle time is set too slow. Correct it to the machine's design speed.
What is the difference between OEE and TEEP?
OEE measures performance during planned production time. TEEP measures it against all calendar time (24 hours, 7 days), so it shows unused capacity as well as losses.
Should planned maintenance be included in the OEE calculation?
Most plants treat scheduled maintenance as planned stop time and exclude it from planned production time. Either approach works if you apply it consistently. Unplanned repairs always count as downtime.
How can I calculate OEE in Excel?
Enter planned production time, downtime, ideal cycle time, total count and good count, then calculate run time, availability, performance, quality and OEE with the formulas in the template above.